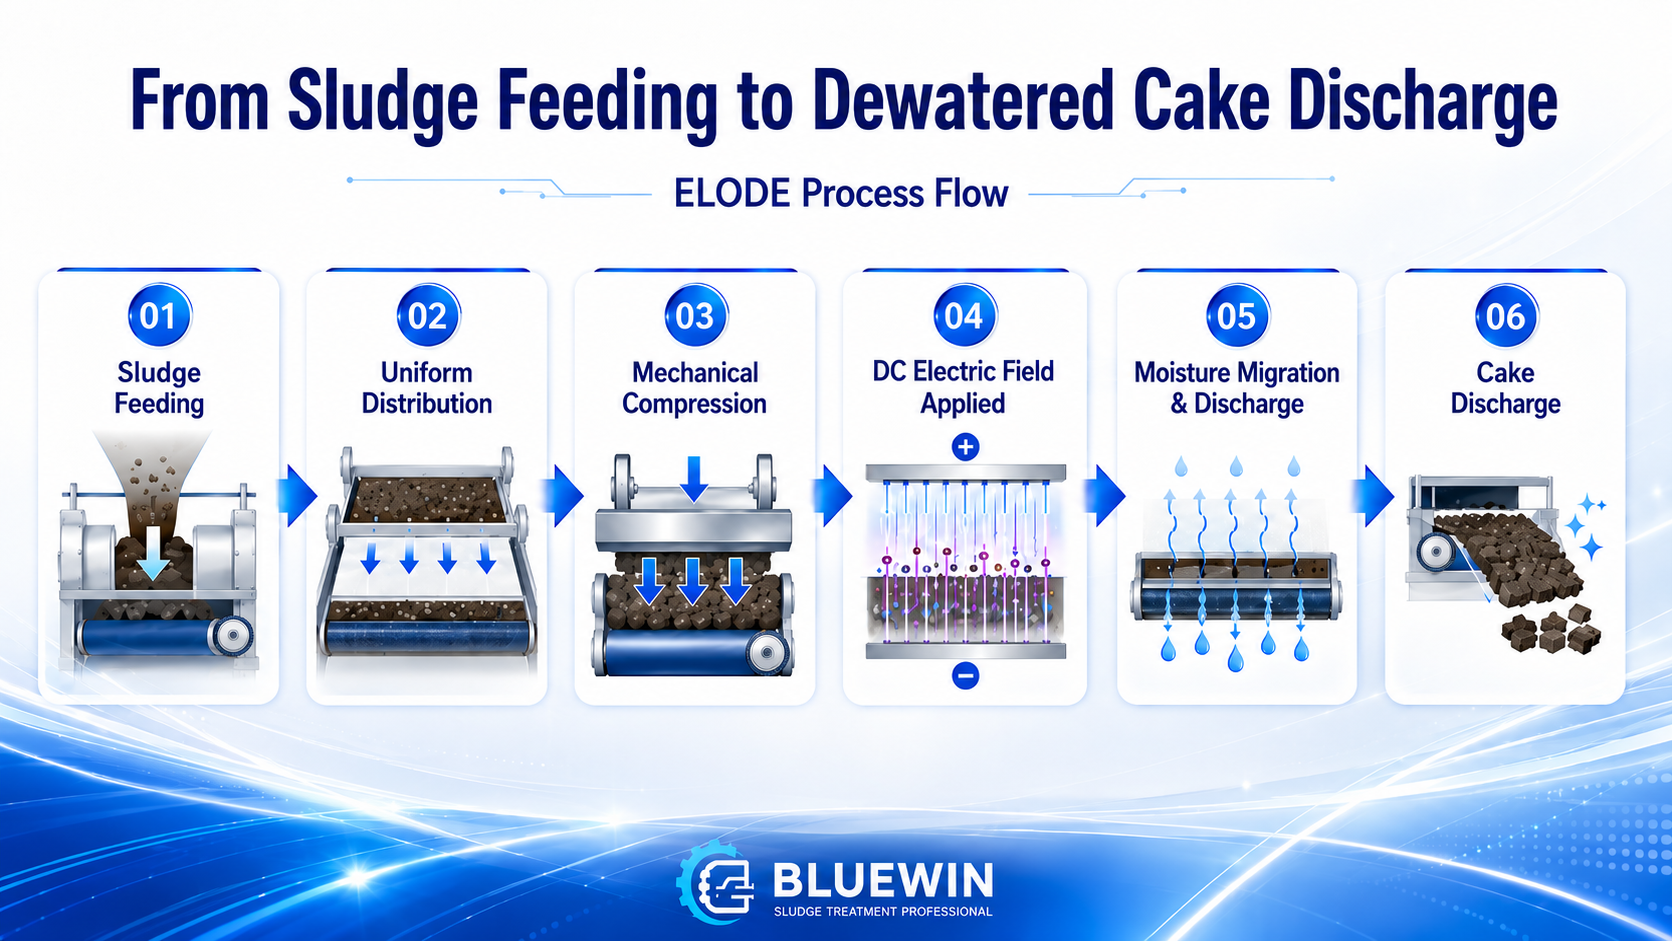
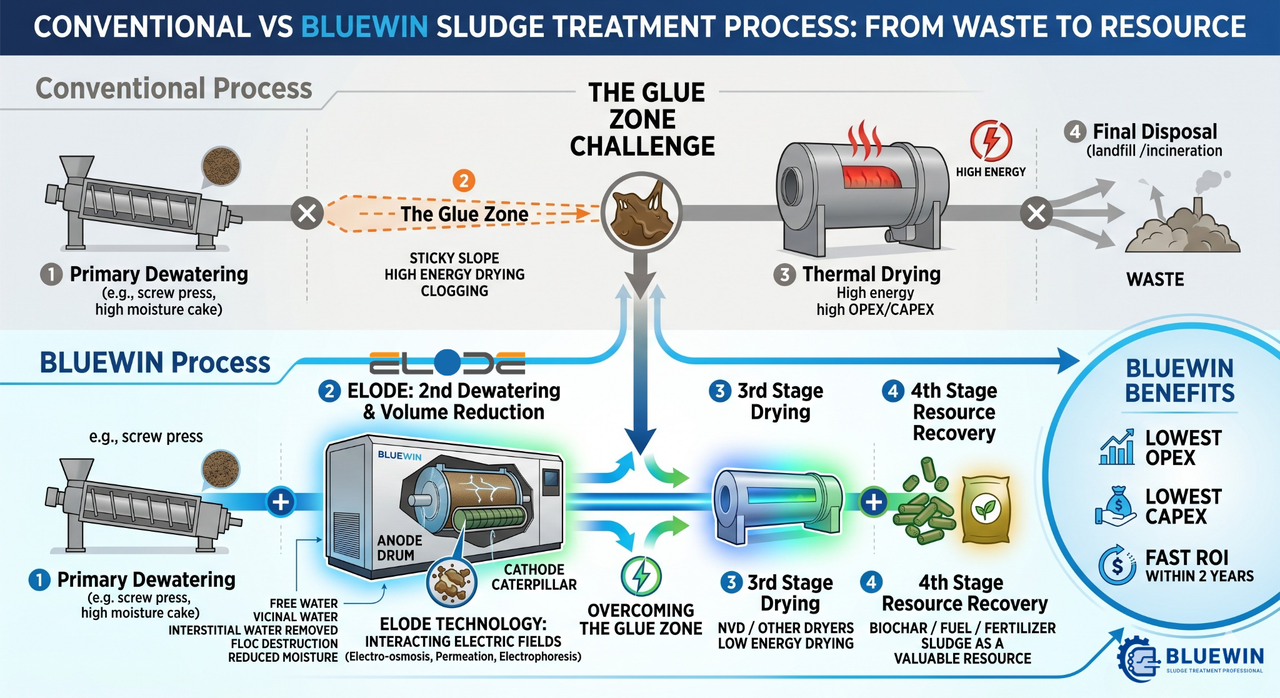
ELODE is an advanced secondary dewatering and sludge reduction system designed to further dewater sludge that has already undergone primary dewatering using conventional equipment such as belt presses, filter presses, or centrifuges.
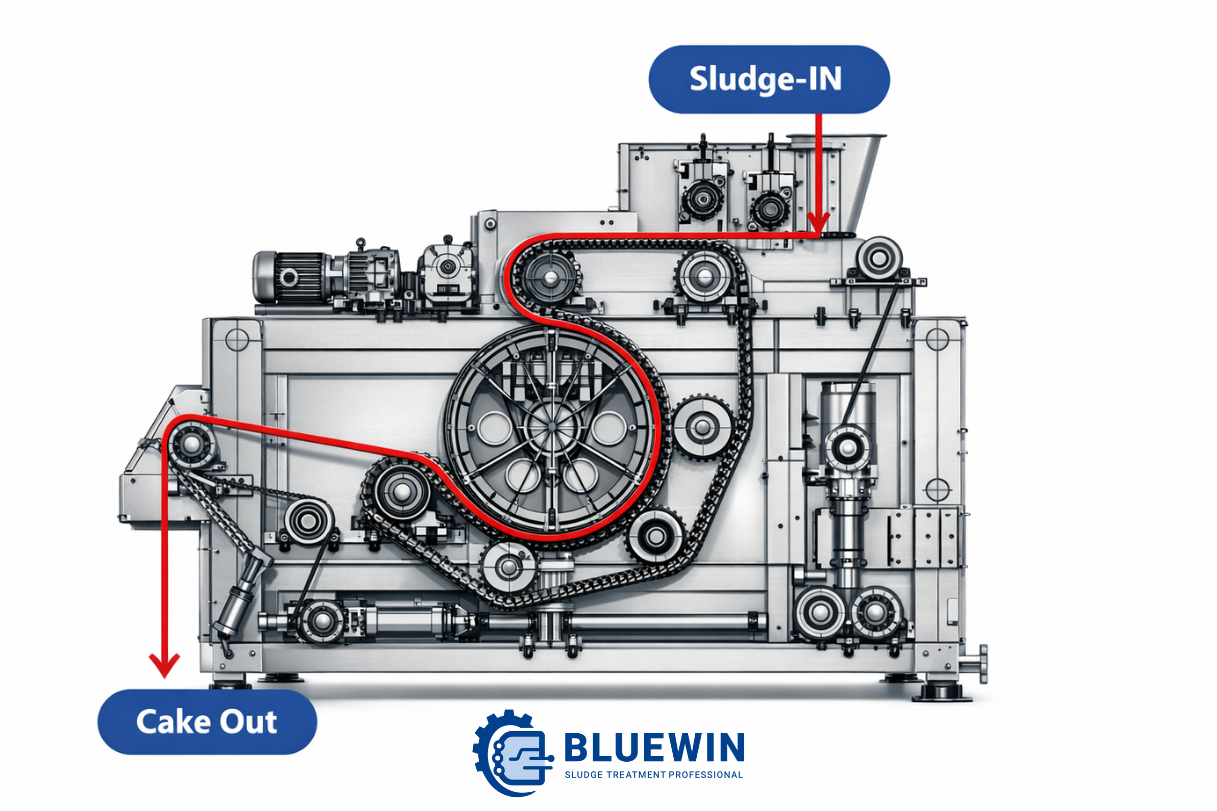
The incoming sludge is evenly distributed at a controlled width and thickness by an automatic sludge distribution system. It then passes between the belt and rollers, where it is subjected to progressive mechanical compression.
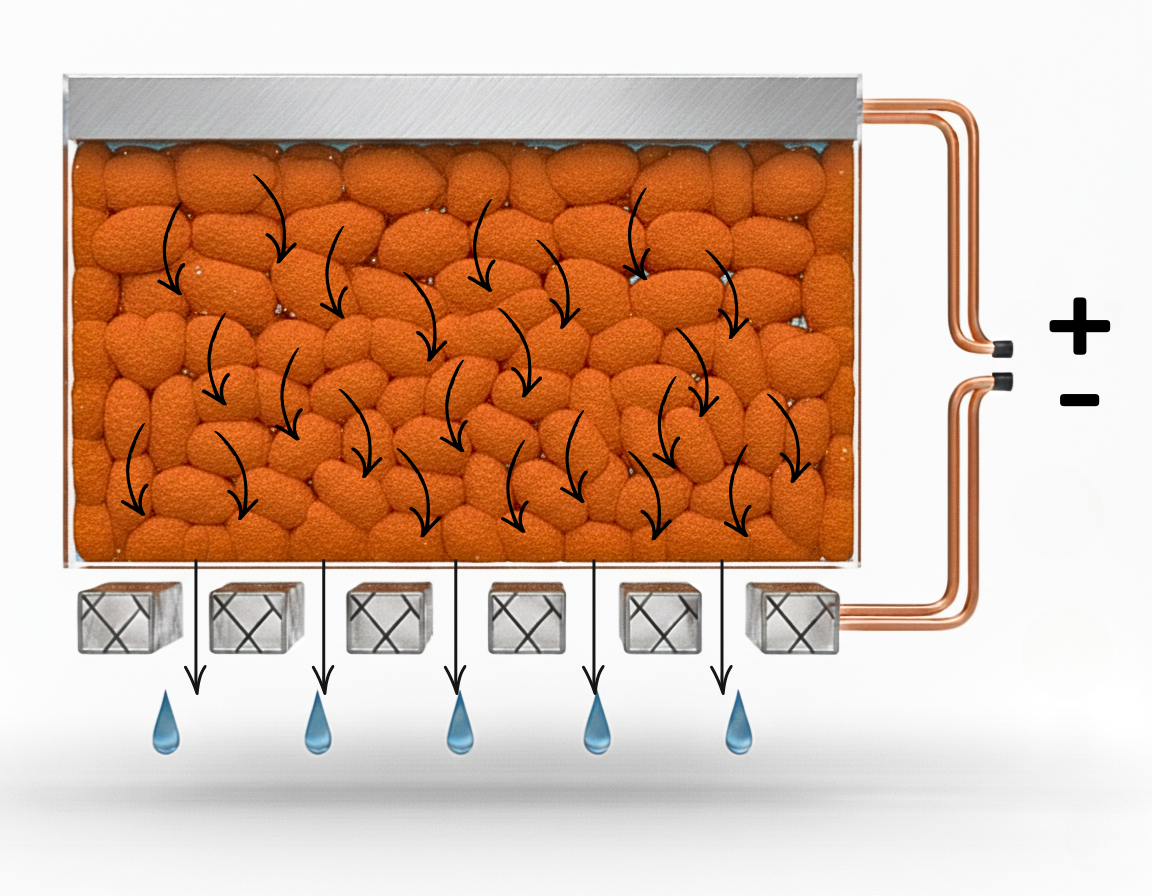
At the same time, a stable DC electric field is applied across the sludge layer, inducing the movement of moisture and charged particles within the sludge.
Through the combined effects of mechanical compression, electro-osmosis, electro-infiltration, and electrophoresis, the separated water is discharged through the belt and the internal drainage structure.
The treated sludge is continuously discharged in the form of a dewatered cake with significantly reduced moisture content and volume.
Reducing the moisture content from
Sludge Drying
Core Technologies
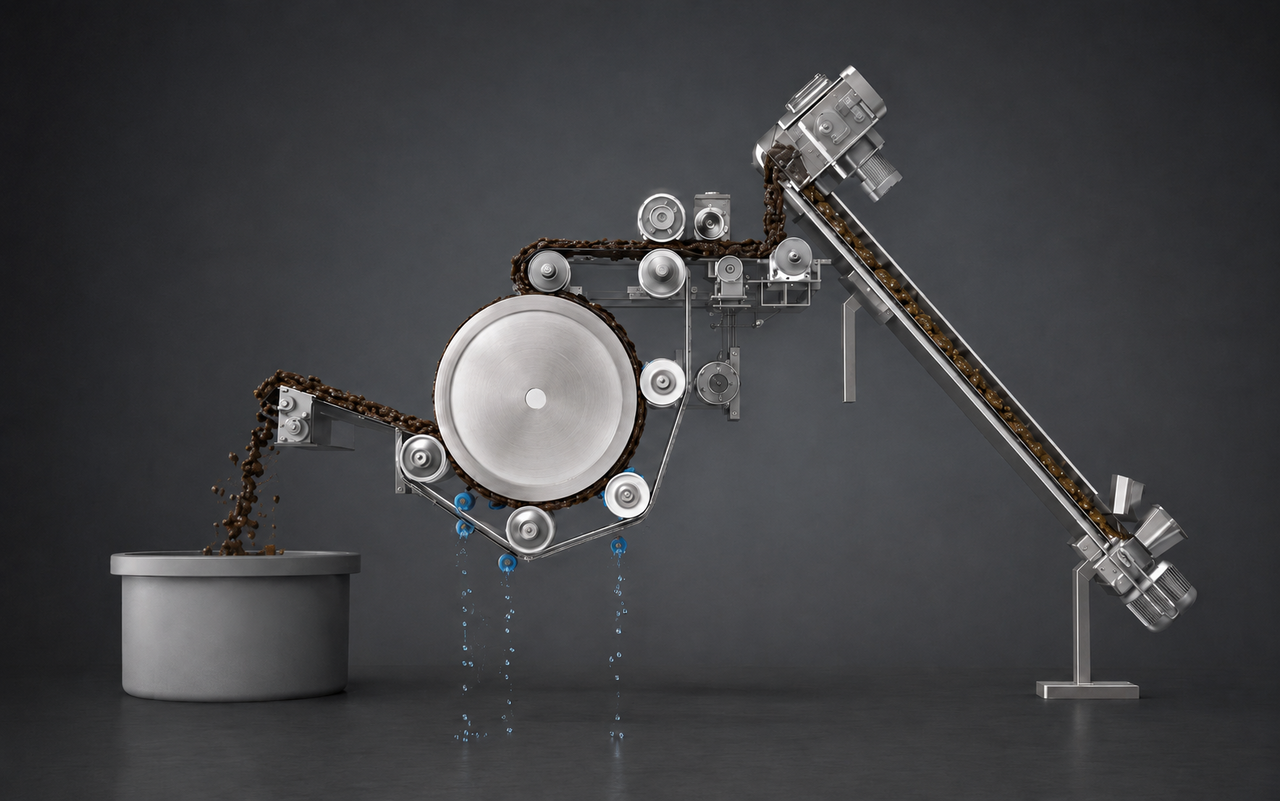
Rather than applying intense pressure at a single point, the system increases the pressure progressively along the sludge travel path. This minimizes disruption and uneven flow within the sludge layer, creating stable and consistent dewatering conditions.
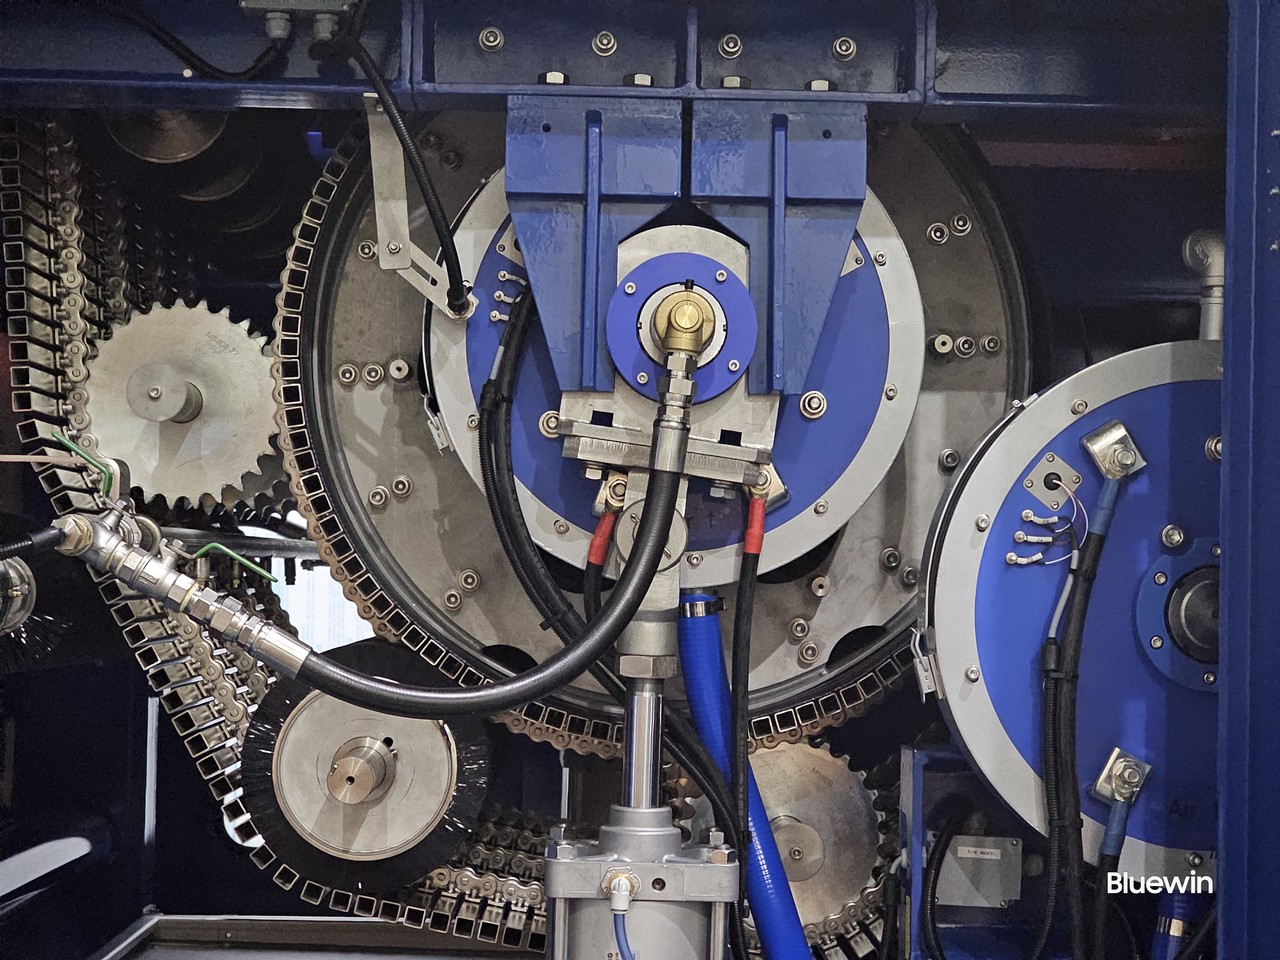
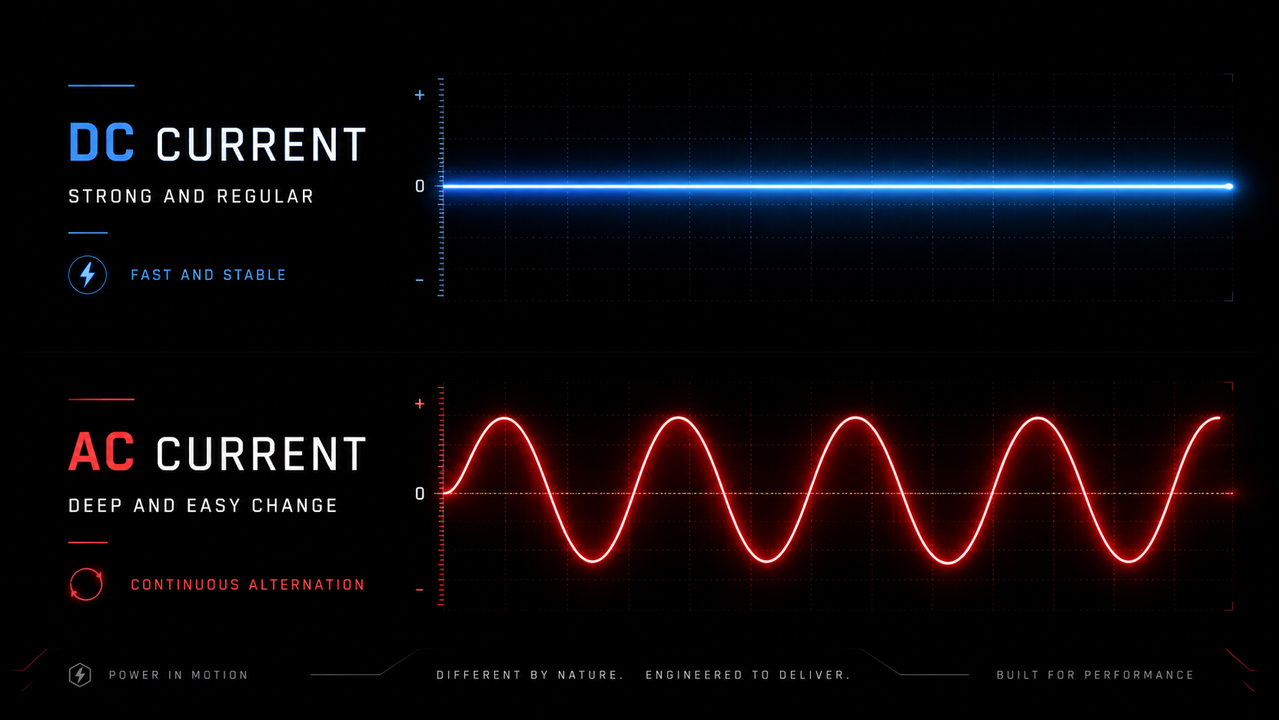
During this process, electro-osmosis, electro-infiltration, and electrophoresis occur simultaneously. While mechanical compression applies physical force from the outside of the sludge layer, these electrical effects promote the movement of moisture and particles from within the sludge structure.
The separated water migrates toward the electrodes and along the belt drainage pathways before being discharged from the sludge layer.
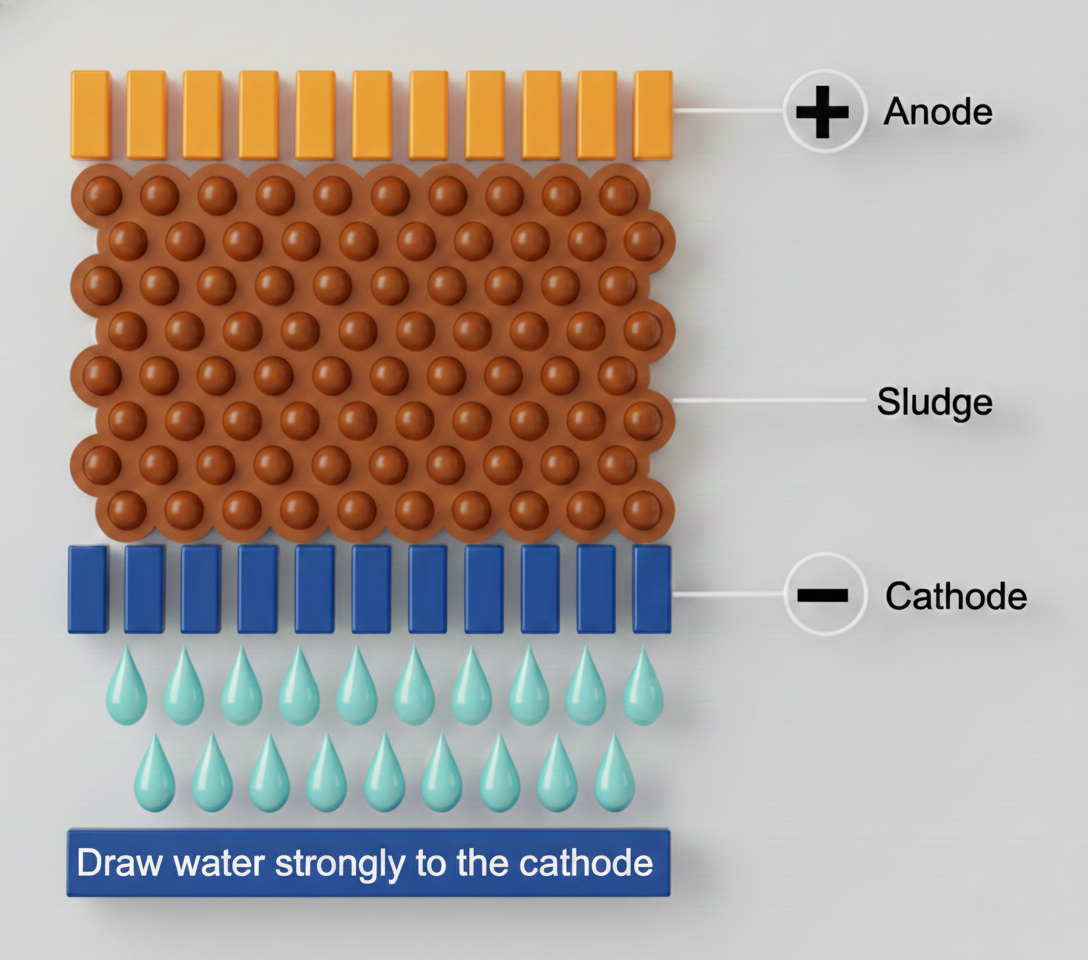
BLUEWIN ELODE is a patented sludge dewatering system in which three electrical mechanisms, electro-osmosis, electro-infiltration, and electrophoresis, act simultaneously.
These combined electrical effects break down the sludge floc structure and rapidly release free water, interstitial water, and intracellular moisture that had previously been trapped or bound within the sludge.
Through this integrated electrical process, ELODE effectively separates internal moisture that is difficult to remove through mechanical compression alone, while consuming only a small amount of electrical energy.
As a result, ELODE delivers highly efficient dewatering performance by rapidly extracting moisture from the sludge within a treatment time of approximately 90 seconds.
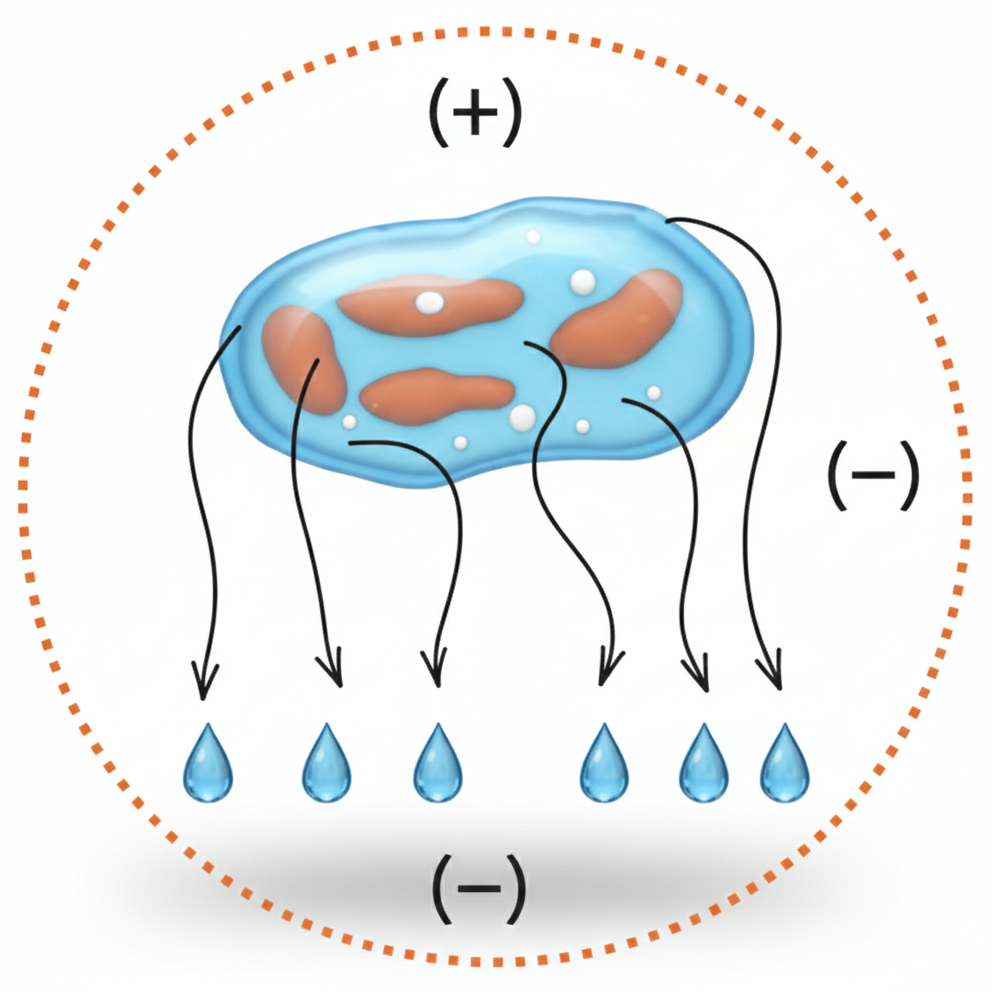
Electro-Osmosis
Using a DC electric field, electro-osmosis drives moisture present on the surfaces of sludge particles and within fine pores in a consistent direction. This enables free water and interstitial water trapped within the floc structure, which are difficult to remove through mechanical compression alone, to migrate rapidly toward the electrodes and drainage pathways.
Electro-Infiltration
Working in combination with mechanical compression, electro-infiltration acts deep within the sludge flocs and fine pores to promote the movement of moisture that is trapped or bound inside the sludge structure. Even as the pores become narrower during compression, it continuously drives the released moisture along the drainage pathways and out of the sludge layer.
Electrophoresis
ELODE uses the electric field to induce the movement and rearrangement of electrically charged fine sludge particles and colloidal substances. This process breaks down the aggregated floc structure and creates pathways through which moisture trapped between the particles can migrate, thereby promoting the separation of solids and water.
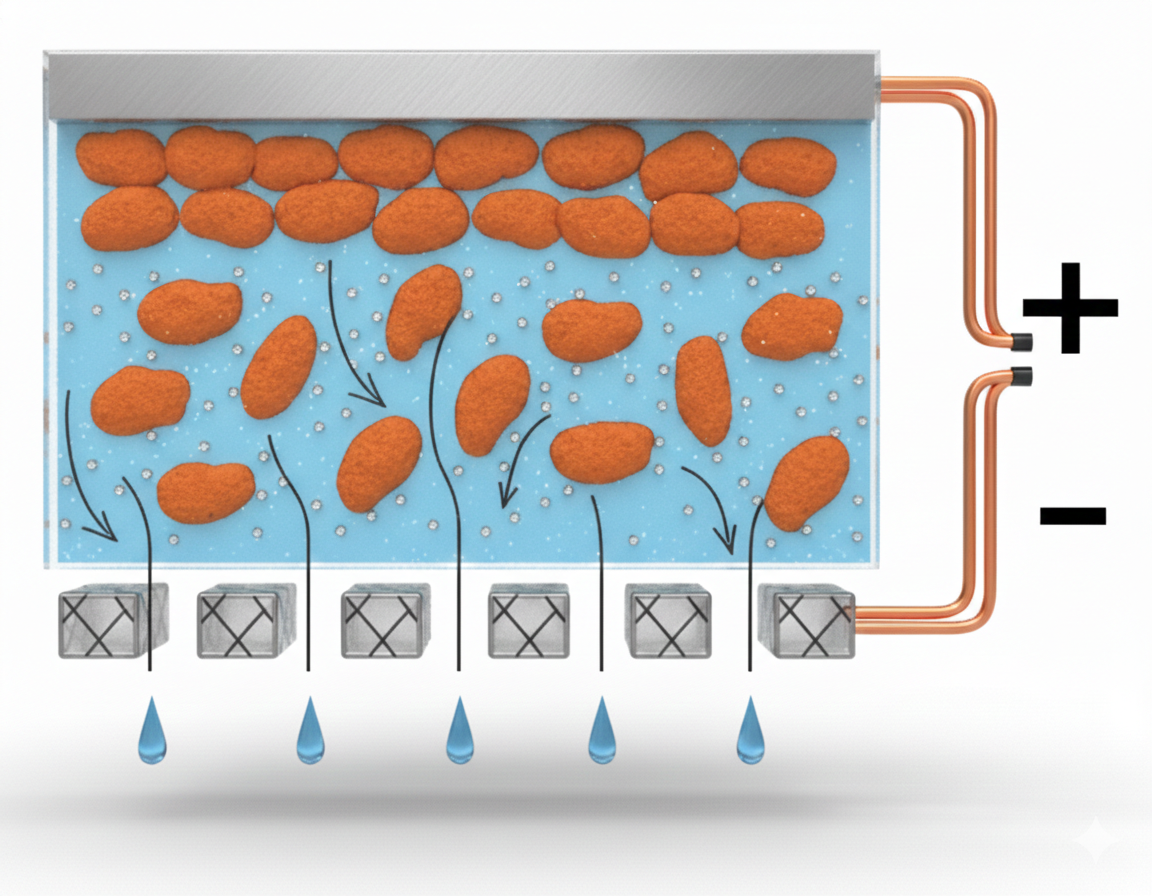
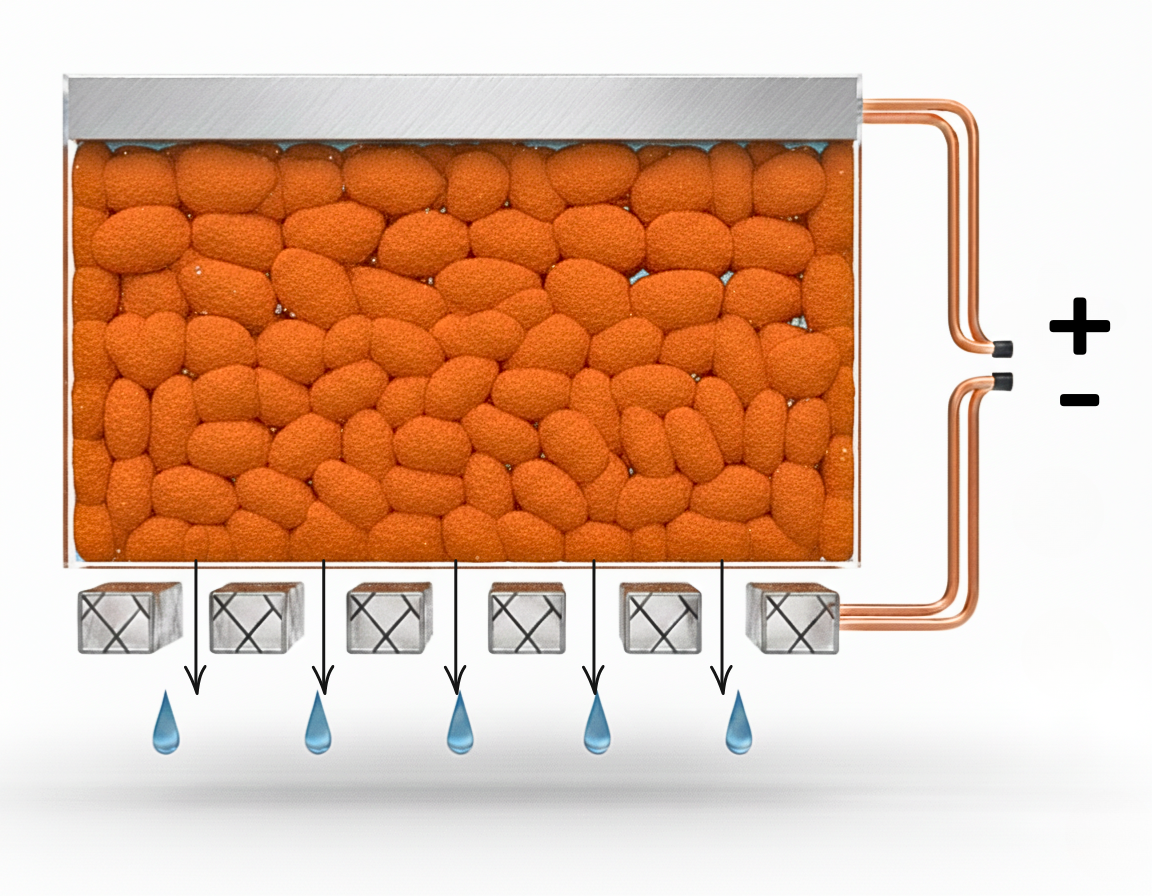
In general, sludge cake produced by primary dewatering forms a highly cohesive structure due to polymer flocculants, high viscosity, and the presence of various organic substances. In addition, sludge particles contain a substantial amount of moisture that is difficult to remove through physical compression alone, including intracellular water and water bound between particles. As a result, conventional mechanical dewatering has inherent limitations in further reducing sludge moisture content.
To remove this difficult-to-dewater moisture, conventional treatment systems have primarily relied on thermal drying. However, thermal drying systems consume large amounts of energy and may generate dust, odors, and exhaust gases during operation. Consequently, additional dust collection, deodorization, and exhaust gas treatment facilities are often required.
The high adhesiveness of sludge within the Glue Zone can also cause sludge to stick to the internal walls and conveying components of the dryer. This may result in clogging, uneven drying, and reduced treatment efficiency. Frequent cleaning, component replacement, and scheduled maintenance are therefore required, increasing both operating costs and maintenance demands.
When dried sludge is intended for use as fuel or as a recoverable resource, consistent moisture content and product quality must also be maintained. If sufficient demand for reuse cannot be secured, additional costs may arise from incineration or other disposal methods.
Conventional sludge drying technologies, including solar drying systems, low-temperature dryers, rotary kilns, drum dryers, fluidized-bed dryers, and thin-film dryers, share several operational limitations. These include high energy consumption, long treatment times, large installation footprints, difficulties in conveying adhesive sludge, and high maintenance costs.
On average, more than 1.0 kWh of energy is required to remove one liter of water.
Dust and Chemical Emissions
Dust and gases generated during the drying process require additional equipment, such as dust collectors and gas scrubbing systems.
Large Installation Footprint
High operating costs (OPEX), substantial initial capital investment (CAPEX), and a large installation area are required.
Corrosion and Scale Formation
Chemical gases can cause corrosion and scale buildup inside the equipment, potentially shortening its service life.
Accumulation of Organic Residues
Sticky organic residues increase maintenance costs and reduce overall operating efficiency.
ELODE addresses the Glue Zone first, maximizing the efficiency of the thermal drying process.
ELODE uses its electrical dewatering technology to pre-treat the Glue Zone, a high-moisture, highly adhesive stage that is difficult to handle efficiently using conventional thermal dryers alone.
By reducing the moisture content and weight of the sludge before it enters the thermal dryer, ELODE lowers the evaporation load while minimizing drying time and energy consumption.
ELODE handles the Glue Zone, while the thermal dryer completes the final drying stage. By combining the most suitable technology for each stage, this integrated solution reduces energy consumption and equipment load while maximizing overall drying efficiency.
 + Rotary Kiln Dryer
Uses high temperatures to rotate and quickly evaporate water from sludge.
+ Drum DryerDelivers stable drying at medium temperatures by rotating the drum and removing water.
+ Fluid Bed DryerForms a fluid bed of sludge for uniform water removal and high thermal efficiency.
+ Low Tem DryerProvides stable drying at low temperatures, minimizing energy consumption.
+ High Temp DryerQuickly evaporates moisture using high temperatures for rapid drying.
+ Film DryerSpreads sludge in a thin film to maximize surface area for fast drying.
+ Solar DryerUtilizes solar energy for an eco-friendly, cost-effective drying solution
The Glue Zone: Difficult to Overcome with Conventional Mechanical Compression Alone
After primary mechanical dewatering, sludge becomes increasingly viscous and resistant to further compression as its moisture content decreases. As the sludge particles become more tightly packed and the floc structure is compressed, the moisture inside the sludge becomes more strongly retained on particle surfaces and within fine pores.
In conventional mechanical dewatering processes, moisture removal efficiency may decline sharply as the sludge moisture content decreases from approximately 80% to 60%. BLUEWIN defines this highly adhesive range, in which further dewatering becomes difficult through mechanical compression alone, as the Glue Zone.
Within the Glue Zone, ELODE does not simply apply greater pressure. Instead, it combines mechanical compression with a stable DC electric field. Electrical effects, including electro-osmosis and electrophoresis, promote the movement of moisture and particles within the sludge, allowing the separated water to be continuously discharged through drainage pathways formed during the compression process.
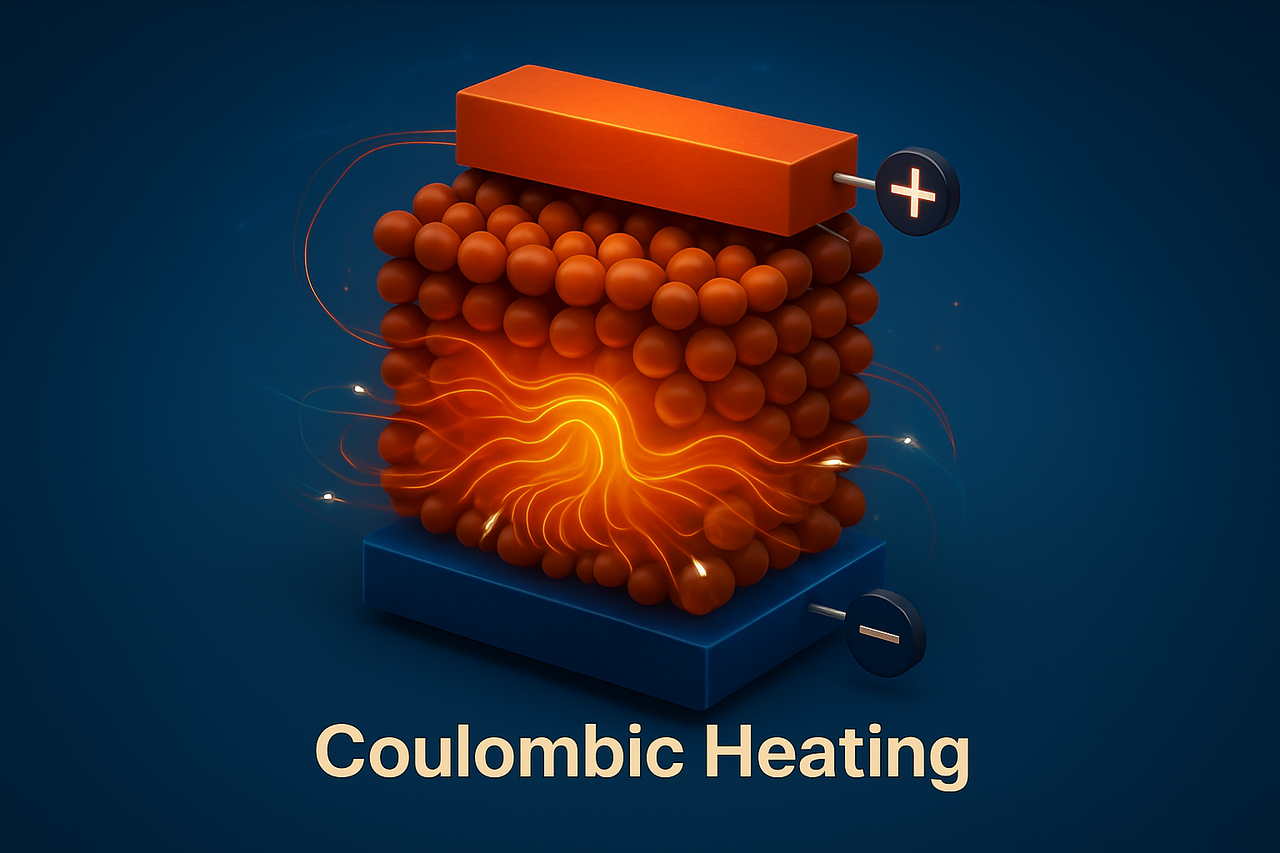
Coulombic Heating Effect: Enhanced Moisture Migration
When DC power is supplied to ELODE, positively and negatively charged ions and particles within the sludge layer migrate rapidly in opposite directions toward their respective electrodes.
During this process, interactions among the charged particles, together with the electrical resistance of the sludge layer, convert a portion of the electrical energy into thermal energy. This phenomenon is referred to as Coulombic heating.
The heat generated within the sludge reduces its viscosity and lowers the resistance to moisture migration. It also weakens the sludge floc structure, allowing free water, interstitial water, and intracellular moisture trapped within the flocs to migrate and separate more easily.
The released moisture is then rapidly discharged through the belt and internal drainage pathways by the combined effects of electro-osmosis, electro-infiltration, electrophoresis, and mechanical compression.
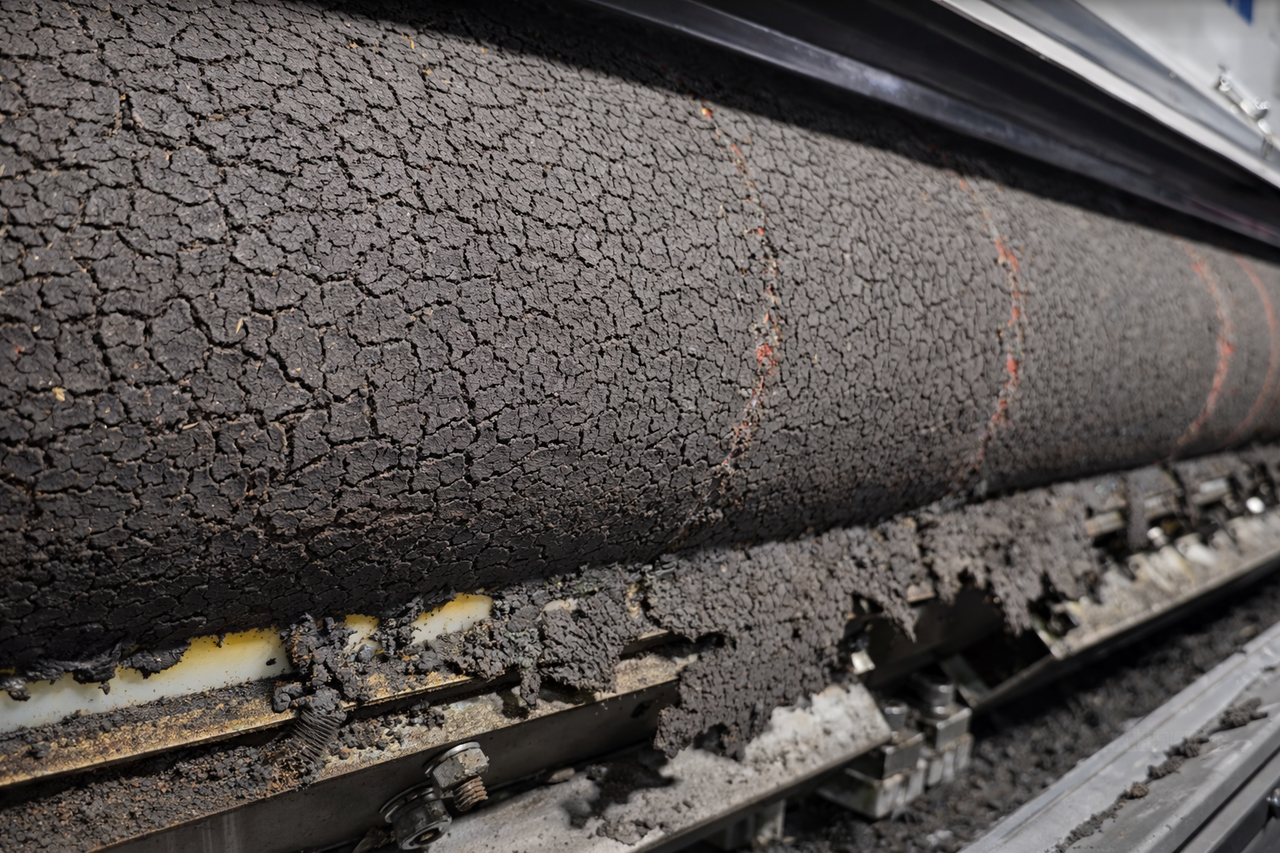
Depending on the sludge characteristics, electrical conductivity, feed rate, and operating conditions, the sludge cake discharged from ELODE may reach a temperature of approximately 40 to 80°C.
Even after the cake leaves the equipment, the residual heat retained within it continues to promote moisture evaporation for a certain period of time, resulting in further moisture reduction after discharge.
RFQ
Contact
© 2025 BLUEWIN Co., LTD. All Rights Reserved.