
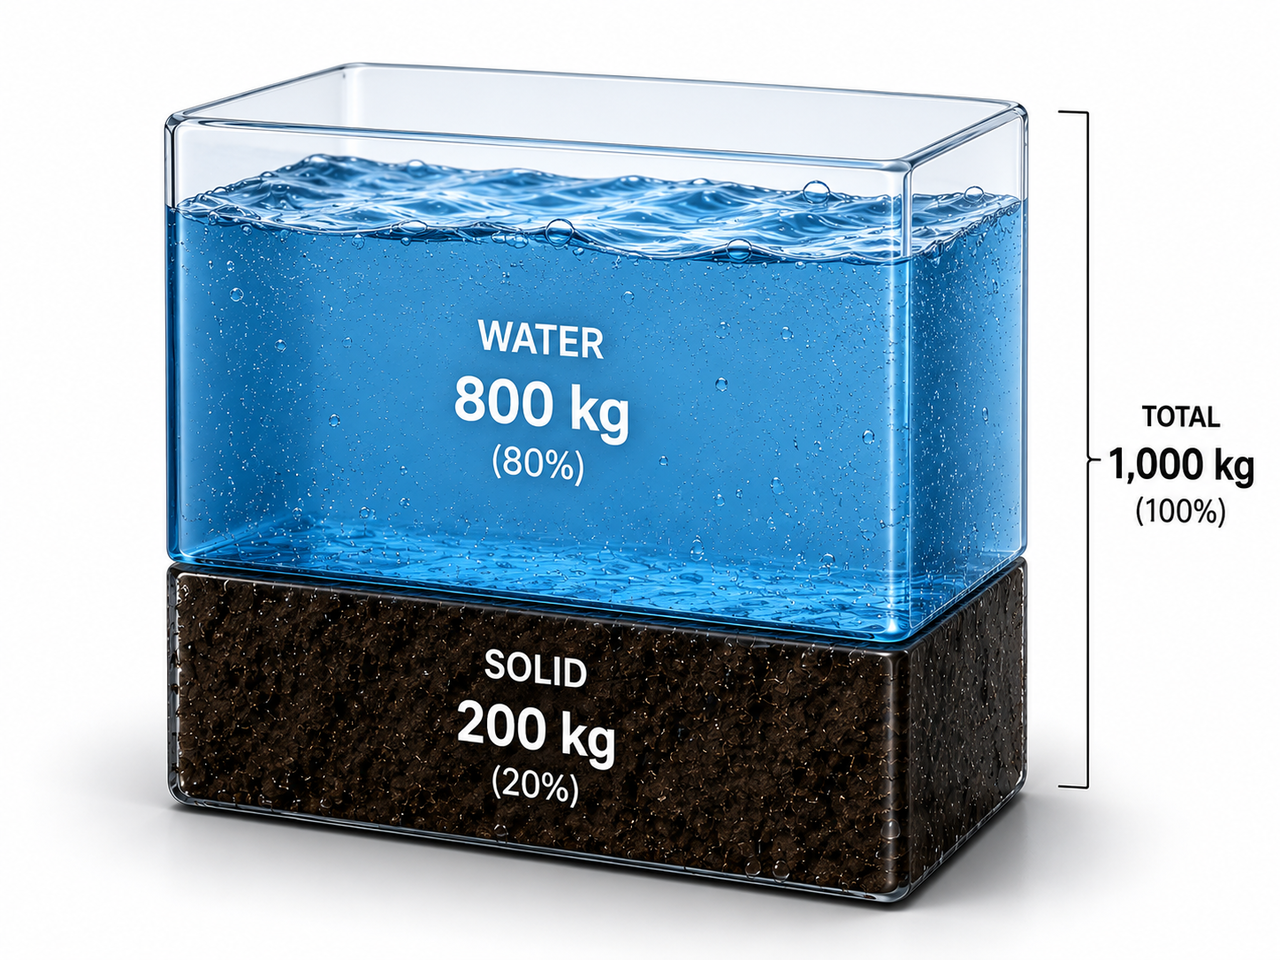
One ton of sludge at 80% moisture content contains approximately 800 kg of water and only 200 kg of dry solids. In other words, a far greater amount of water than the actual solids requiring treatment must be transported, stored, heated, and ultimately removed throughout the sludge treatment process.
The more moisture that remains in the sludge, the greater its total weight and volume become. This increases the number of transportation trips required and the associated fuel consumption, while also expanding the capacity requirements for storage and conveying systems, as well as the overall installation footprint.
In downstream drying processes, more water must be evaporated, resulting in higher consumption of electricity and thermal energy. At the same time, the required capacity and operational burden of the dryer and auxiliary systems, including ventilation, dust collection, odor control, cooling, and material conveying equipment, also increase.
A larger volume of final sludge also requires more energy and higher treatment costs for incineration, landfilling, off-site transportation, or resource recovery.
Therefore, the water contained in sludge is not simply moisture. It is a hidden burden that simultaneously increases transportation costs, drying costs, equipment investment, disposal expenses, and carbon emissions.
Before the downstream treatment stage, ELODE removes additional residual moisture that is difficult to extract through conventional mechanical dewatering. By reducing the moisture content and total weight of the sludge in advance, ELODE significantly improves the efficiency of the entire downstream process.
This reduces the downstream drying load, required equipment capacity, operating time, installation footprint, transportation volume, and final disposal quantity. As a result, ELODE structurally reduces energy consumption and the carbon footprint across the entire sludge treatment process.
To reduce carbon emissions from sludge treatment, we must transport less water, heat less water, and process less water.
1. Transportation
Increased weight · More transportation trips · Higher fuel consumption
2. Energy
Increased drying load · Higher electricity consumption · Longer operating time
 3. Equipment
Larger dryer capacity · Expanded auxiliary equipment
 4. Space
Larger installation footprint · Increased storage space
 5. Treatment Costs
Higher transportation, drying, and disposal costs
 6. Carbon Emissions
Increased emissions throughout transportation, operation, and final disposal
There are two primary methods of removing moisture from sludge.
Conventional thermal dryers remove water by heating and evaporating it. In contrast, ELODE uses electro-osmosis combined with mechanical pressure to separate and discharge moisture while it remains in a liquid state.
Evaporating water inherently requires a substantial amount of thermal energy.
ELODE, however, removes as much separable moisture as possible before the energy-intensive evaporation stage. This reduces the moisture load on the downstream dryer and lowers the overall energy consumption of the sludge treatment process.
Theoretical Energy Required for Water Evaporation
Energy required to heat and completely evaporate 1 liter of water
Approximately 640 kcal ≈ 0.74 kWh
This represents the theoretical minimum thermal energy required at atmospheric pressure to heat 1 liter of water from 0°C to 100°C and then completely evaporate it.
In an actual thermal drying process, energy consumption may be significantly higher due to the additional energy required to heat the sludge and equipment, compensate for heat losses, and operate auxiliary systems.
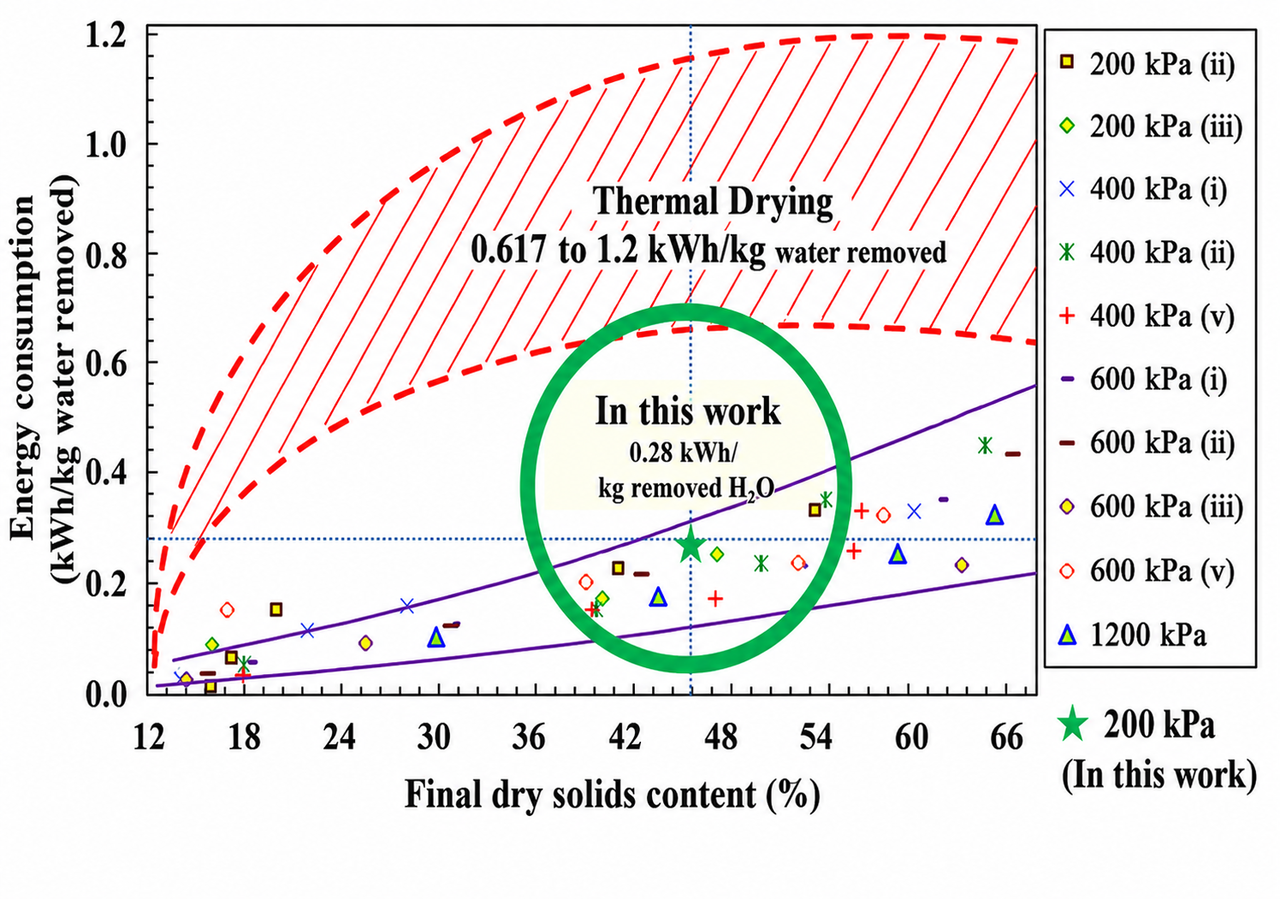
1. Conventional Thermal Drying
Thermal Drying
Although these drying technologies differ in equipment configuration, operating temperature, and heat source, they all fundamentally remove moisture by heating and evaporating the water contained in sludge.
Key Characteristics
Key Energy Consumption Range
Approximately 0.617 to 1.20 kWh per kg of water removed
2. ELODE Water Separation
ELODE does not remove moisture by heating or evaporating it.
Instead, ELODE simultaneously applies a precisely controlled direct-current electric field and mechanical pressure to the sludge layer, inducing the following three electrokinetic mechanisms:
The combined action of these mechanisms promotes the movement of moisture trapped within sludge flocs and cellular structures. This enables ELODE to separate and discharge residual moisture in liquid form, including water that is difficult to remove through conventional mechanical dewatering alone.
By removing as much separable moisture as possible before the energy-intensive evaporation stage, ELODE reduces the moisture load on downstream dryers and lowers the total energy consumption of the sludge treatment process.
Key Benefits
Key Energy Consumption Range
Approximately 0.25 to 0.45 kWh per liter of water removed
100 tons of sludge at 80% moisture content contains approximately 20 tons of dry solids and 80 tons of water. To reduce the final moisture content to 10% while maintaining the same amount of dry solids, approximately 77.78 tons of water must be removed per day.
100 tons/day
Daily Sludge Input
80% MC (= 20% DS)
Inlet Moisture Content
10% MC (= 90% DS)
Target Final Moisture Content
77.78 tons/day
Required Water Removal
ELODE Combination System | Conventional Thermal Drying | |
Daily Water Removal | 77,780 kg/day | 77,780 kg/day |
Energy Consumption per kg of Water Removed | 0.30 kWh/kg-H₂O | 1.00 kWh/kg-H₂O |
Daily Energy Consumption | 23,334 kWh/day | 77,780 kWh/day |
Daily Energy Savings | 54,446 kWh/day | |
Energy Reduction | Approx. 70% |
Under the same sludge treatment capacity and target moisture content, the ELODE Combination System can save approximately 54,446 kWh of energy per day, representing an energy reduction of approximately 70% compared with conventional thermal drying.
Assuming 330 operating days per year and an electricity emission factor of 0.5 kgCO₂e/kWh, the annual energy savings would amount to approximately 17,967,180 kWh, corresponding to an estimated annual carbon reduction of approximately 8,983 tCO₂e.
Carbon Reduction Calculation
54,446 kWh/day × 330 days/year × 0.5 kgCO₂e/kWh ÷ 1,000
= Approx. 8,983 tCO₂e/year
Based on the same electricity emission factor, this represents an approximately 70% reduction in electricity-related carbon emissions compared with conventional thermal drying.
In addition, the ELODE Combination System reduces the volume and weight of sludge before it enters the downstream drying process. This can lower not only electricity consumption and operating costs, but also the carbon footprint associated with sludge dewatering, drying, transportation, and final disposal across the entire treatment process.
*Annual CO₂ emissions reduction is an estimated value calculated based on a daily energy saving of 54,446 kWh, 330 operating days per year, and an electricity emission factor of 0.5 kgCO₂e/kWh.
Reduced energy consumption directly lowers electricity and fuel costs. It also reduces the load and operating time of downstream drying processes, as well as the volume of sludge requiring transportation and final disposal, thereby lowering overall operating costs.
Where carbon taxes, emissions trading schemes, or internal corporate carbon pricing mechanisms apply, the resulting reduction in carbon emissions can be converted into additional economic value.
1. Energy Cost Savings Are Immediate
Energy Cost Savings = Energy Savings × Electricity or Thermal Energy Rate
For example, if the electricity rate is USD 0.12/kWh:
These are direct operating cost savings that occur regardless of whether a carbon pricing scheme is applied. As energy consumption decreases, electricity and fuel costs are immediately reduced.
These savings accumulate throughout the operating period, lowering the overall treatment cost and shortening the payback period.
2. Reduced Carbon Emissions Create Additional Economic Value
For projects subject to carbon credits, carbon taxes, internal carbon pricing, or customers’ ESG cost criteria, carbon reduction can be converted into direct economic value.
Carbon Cost Savings = Carbon Reduction × Applicable Carbon Price
For example:
Actual carbon cost savings may vary depending on the project country, applicable carbon tax or emissions trading price, regulatory requirements, and the company’s internal carbon pricing policy.
3. Cost Savings Extend Across the Entire Process
The economic benefits of ELODE are not limited to electricity and carbon-related costs.
Carbon reduction is not merely an environmental indicator. By lowering energy and resource consumption, it reduces costs across the entire process and ultimately contributes to both CAPEX and OPEX savings.
The table below compares the sludge generation, energy costs, disposal costs, and carbon-related costs of a conventional process consisting of mechanical dewatering followed by thermal drying with those of the ELODE Combination System, under the same treatment capacity and operating conditions.
The ELODE Combination System increases the final dry solids content to approximately 80%, reducing annual sludge cake generation from approximately 9,450–10,500 tons under the conventional process to approximately 2,352 tons.
As a result, the total amount of sludge generated can be reduced by approximately 75–78%, while simultaneously lowering thermal drying energy consumption, carbon emissions, transportation costs, and final disposal costs.
Index | Before ELODE+NVD | After ELODE+NVD | |||
|---|---|---|---|---|---|
Application 1st stage Dewatering Mechanical machine | CENTRIFUGE Dewatering Machine | BELTPRESS | FILTERPRESS | SCREWPRESS | EODS-3000+NVD-3000*1set |
| Throughput | 15m³/hr @1.5%ss | 15m³/hr @1.5%ss | 15m³/hr @1.5%ss | 15m³/hr @1.5%ss | 15m³/hr @1.5%ss get 18%ds from 1st Mechanical Dewatering M/C → Inlet 1.25 ton/hr |
| Model and 1set | KOWATS-360 D | AKI-BFS-2000 | FB-500 | KOWATS-500SP | EODS-3000+NVD-3000* |
| Electric consumption | 50kW | 15kW | 10kW | 5.5kW | 300kW |
| Dry Solid | 20% | 18% | 18% | 20% | 80% |
| CAKE Out Volume/year | 1.125 ton × 24 hr × 350 days = 9,450 ton | 1.25 ton × 24 hr × 350 days = 10,500 ton | 1.25 ton × 24 hr × 350 days = 10,500 ton | 1.125 ton × 24 hr × 350 days = 9,450 ton | 0.28 ton × 24 hr × 350 days = 2,352 ton |
| ① Sludge Disposal fee/ton.year | $1,134,000 | $1,260,000 | $1,260,000 | $1,134,000 | $0 |
| ② CO2 Emission cost for generated when sludge is incinerated to get 80%ds (or using Thermal dryer) | 7,087,000 liter water × 0.98kW energy needs = 6,945,260 kW × 0.5kg = 3,472 ton CO₂ × $65 = $225,680 | 8,137,500 liter water × 0.98kW energy needs = 7,974,750 kW × 0.5kg = 3,987 ton CO₂ × $65 = $259,155 | 8,137,500 liter water × 0.98kW energy needs = 7,974,750 kW × 0.5kg = 3,987 ton CO₂ × $65 = $259,155 | 7,087,000 liter water × 0.98kW energy needs = 6,945,260 kW × 0.5kg = 3,472 ton CO₂ × $65 = $225,680 | 2,520,000 liter water × 0.98kW energy needs = 1,260 ton CO₂ × $65 = $65,520 |
| ③ Energy consumption cost to get 80%ds/year | 6,945,260 kW × $1.2 = $8,334,000 | 7,974,750 kW × $1.2 = $9,569,700 | 7,974,750 kW × $1.2 = $9,569,700 | 6,945,260 kW × $1.2 = $8,334,000 | 2,520,000 kW × $1.2 = $3,024,000 |
The annual carbon reduction of approximately 8,983 tCO₂e has been converted into the equivalent amount of CO₂ absorbed by pine trees.
An annual reduction of approximately 8,983 tons of CO₂e is equivalent to the amount of carbon dioxide absorbed in one year by approximately 1.36 million 30-year-old pine trees.
8,983.59 tCO₂e × 1,000 = 8,983,590 kgCO₂e
8,983,590 kgCO₂e ÷ 6.6 kgCO₂/(tree·year)
= Approx. 1,361,150 trees
≈ Approx. 1.36 million trees
Conventional Thermal Drying | ELODE Combination | Annual Reduction | |
Annual Energy Consumption | 25,667,400 kWh | 7,700,220 kWh | 17,967,180 kWh |
Annual Carbon Emissions | Approx. 12,834 tCO₂e | Approx. 3,850 tCO₂e | Approx. 8,984 tCO₂e |
Equivalent Pine Tree Absorption | Approx. 1.94 million trees | Approx. 580,000 trees | Approx. 1.36 million trees |
Under the same treatment capacity and target moisture content,
the conventional thermal drying process generates approximately 12,834 tCO₂e of greenhouse gas emissions per year due to its electricity consumption,
while the ELODE Combination System generates approximately 3,850 tCO₂e per year.
As a result, the ELODE Combination System can reduce greenhouse gas emissions by approximately 8,984 tCO₂e per year, or about 70%,
compared with conventional thermal drying.
This reduction is equivalent to the amount of carbon dioxide absorbed in one year by approximately 1.36 million 30-year-old pine trees.
The ELODE Combination System becomes increasingly energy-efficient as the equipment size and treatment capacity increase. The following are examples of energy consumption for different ELODE models:
| DEMO EODS-500 Model | |
| Inlet | About 67% Save or Reduction vs General Dryer |
| Total Water Removed | 125 liters |
| Energy Consumption | 50 kWh (initial peak of 60 kWh) |
| Energy Efficiency | 0.40 kW per liter of water removed |
| USA Hendersons wwtp EODS-3000 Model | |
| Inlet | 1250 kg at 80% moisture → Outlet: 625 kg at 60% moisture |
| Total Water Removed | 625 liters |
| Energy Consumption | 200 kWh (initial peak of 220 kWh) |
| Energy Efficiency | 0.32 kW per liter of water removed |
| CHINA Guiyang wwtp EODS-2000 Model | |
| Inlet | 800 kg at 82.51% moisture → Outlet: 271 kg at 48.49% moisture |
| Total Water Removed | 529 liters |
| Energy Consumption | 150 kWh (initial peak of 160 kWh) |
| Energy Efficiency | 0.284 kW per liter of water removed |
| Lotte Chemical EODS-3000+NVD-3000 Combination | |
| Inlet | 1250 kg at 80% moisture → Outlet: 278 kg at 10% moisture |
| Total Water Removed | 972 liters |
| Energy Consumption | 300 kWh (initial peak of 350 kWh) |
| Energy Efficiency | 0.30 kW per liter of water removed |
The ELODE Combination System delivers exceptional energy efficiency and outstanding sludge treatment performance,
producing high-quality sludge cake with minimal energy consumption.
In addition, it reduces the need for supplementary dust collection and cleaning equipment, providing a more sustainable and cost-effective solution for sludge treatment and management.


High-moisture sludge requires a significant amount of energy when it is dried or incinerated without sufficient prior volume reduction, because a large amount of water must first be removed from the sludge. This results not only in higher energy consumption and operating costs, but also in increased carbon emissions throughout the entire sludge treatment process, including transportation, drying, incineration, and final disposal.
The ELODE Combination System combines highly efficient electro-osmotic dewatering with an optimized downstream drying process to effectively reduce sludge moisture content and volume. As a result, it can reduce energy consumption and greenhouse gas emissions compared with conventional thermal drying, while also lowering downstream drying load, operating time, transportation volume, and final disposal costs.
As carbon neutrality becomes a new industrial standard rather than an option, the ELODE Combination System offers a sustainable solution that delivers both environmental and economic value.
Less Energy. Lower Carbon. Greater Efficiency.
Reduce energy use, lower carbon emissions, and improve operational efficiency.


RFQ
Contact
© 2025 BLUEWIN Co., LTD. All Rights Reserved.


