
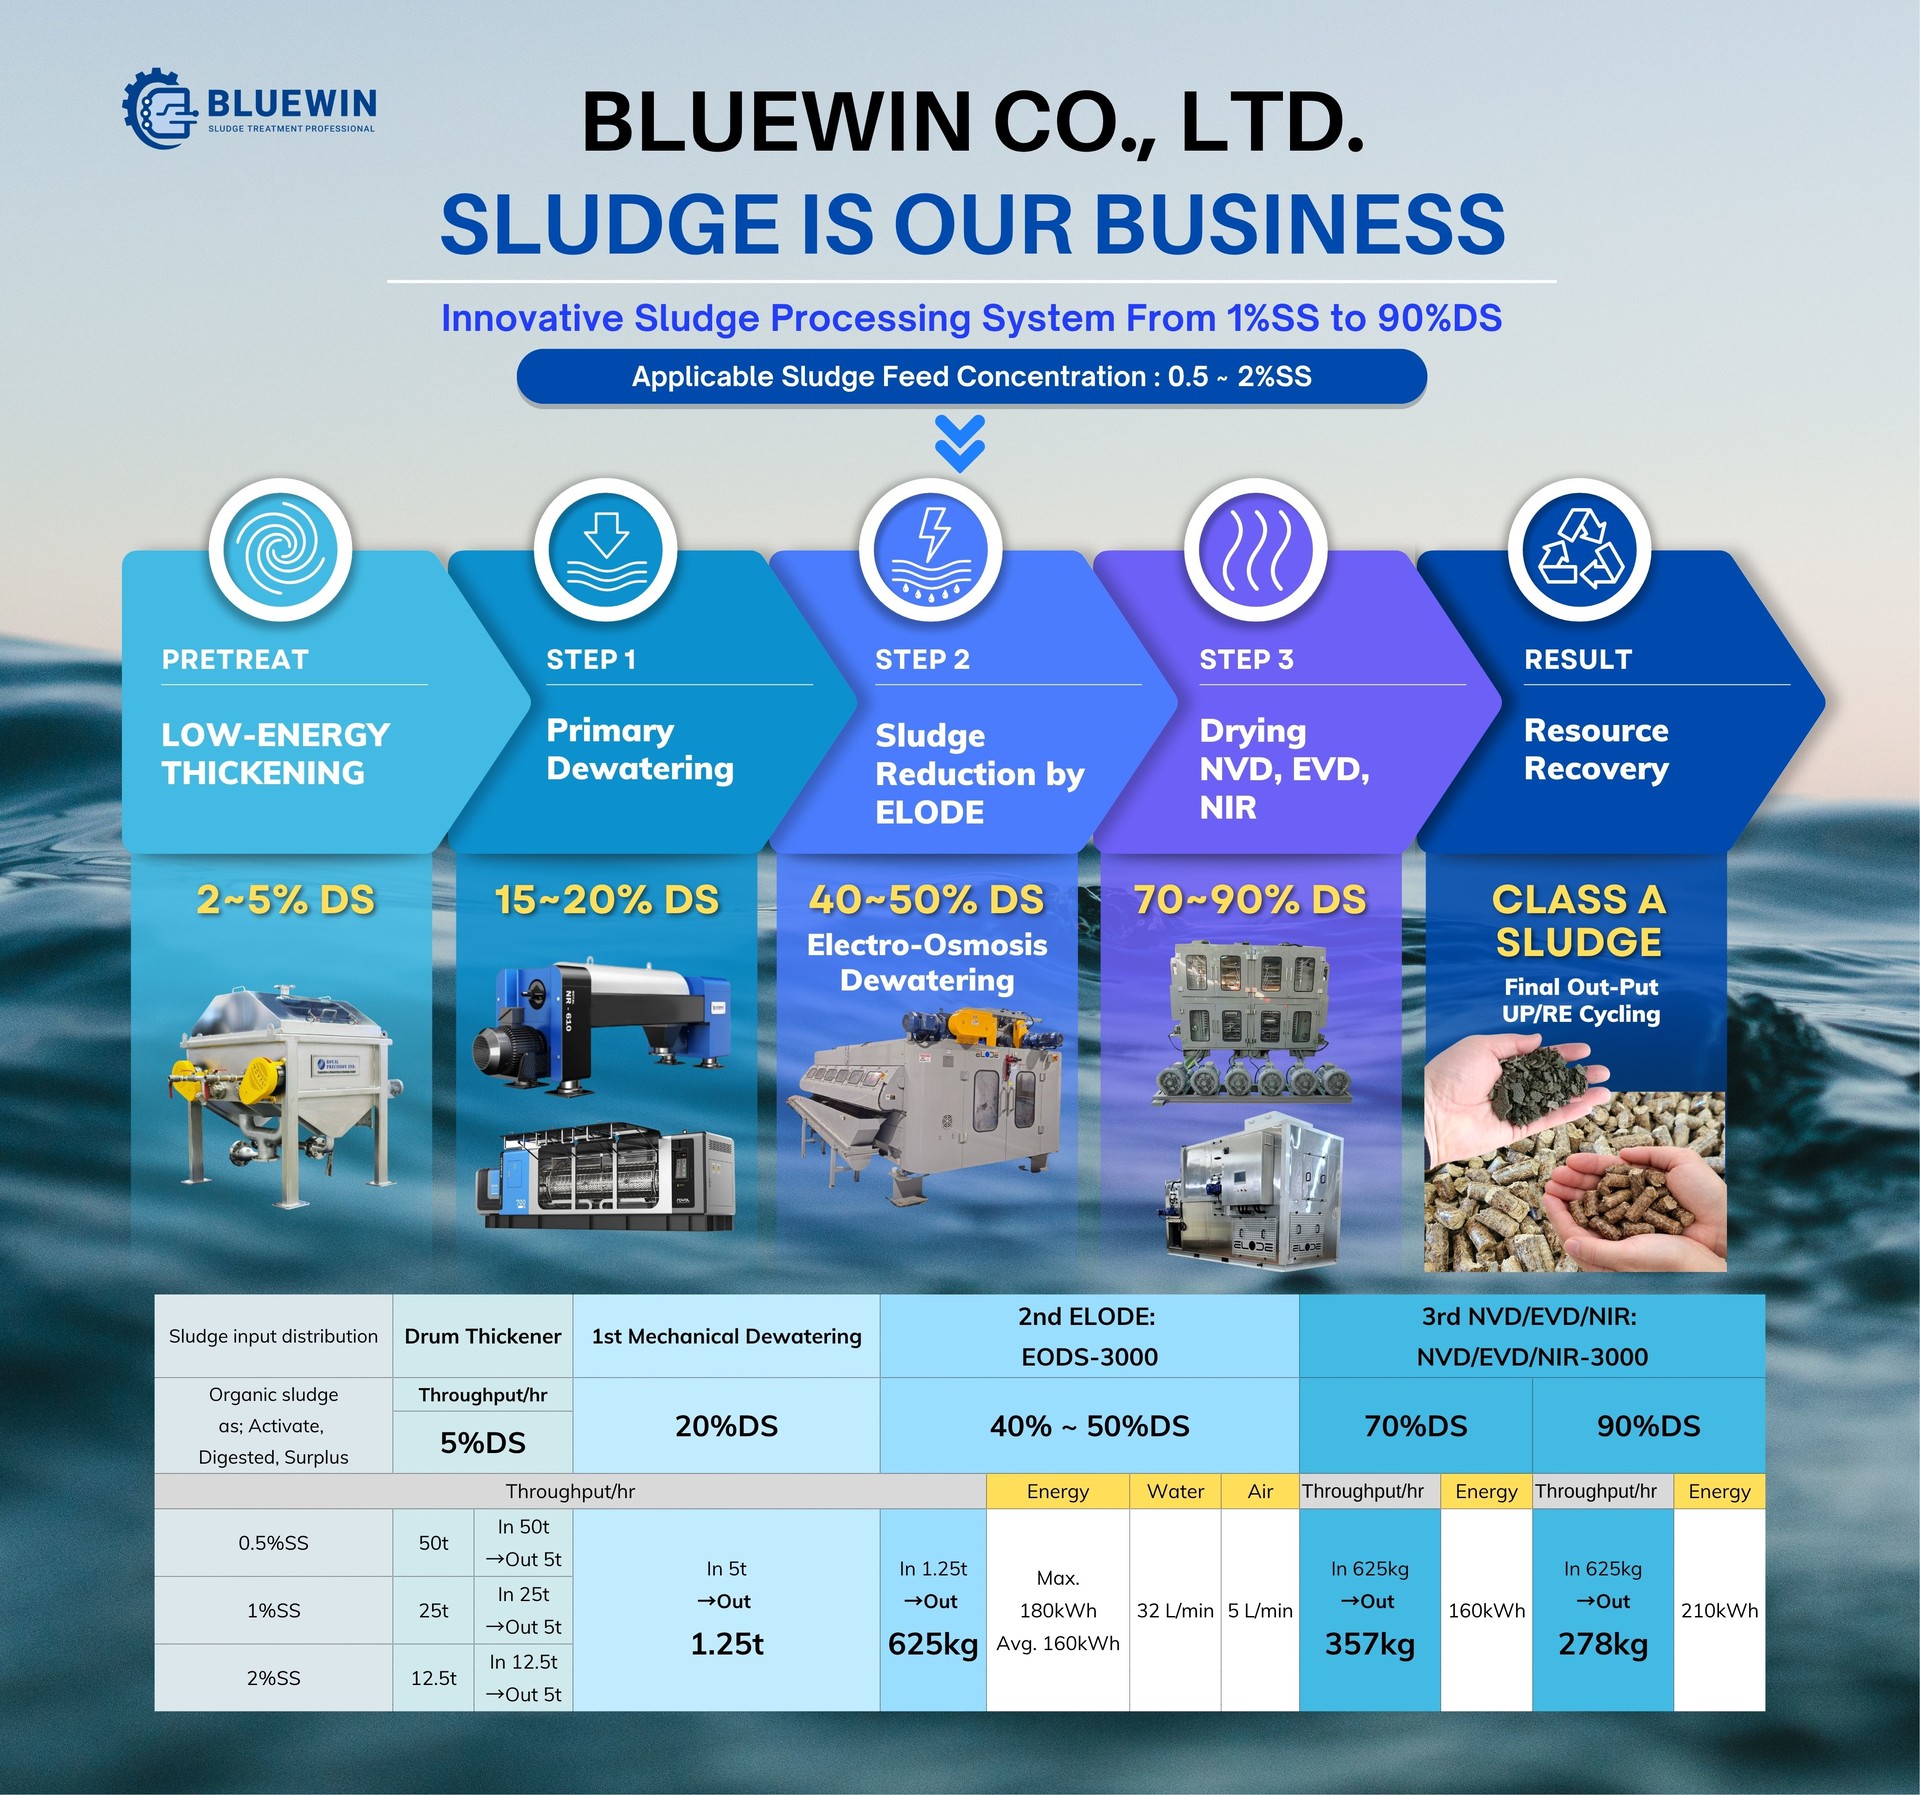
In the moisture-content range of approximately 80% to 60%, sludge enters what is known as the Glue Zone, where it becomes highly viscous, sticky and difficult to handle. In this range, further water removal by mechanical compression alone becomes increasingly difficult, while subsequent thermal drying requires significantly more energy and operating time.
ELODE simultaneously applies three electrokinetic mechanisms:
These three electrical actions destabilize and loosen the sludge floc structure, promoting the release of moisture trapped within the sludge, including free water, interstitial water, bound water and intracellular water. The released moisture is rapidly converted into removable free water and directed toward the discharge side, typically within approximately 90 seconds.
Through this process, ELODE effectively removes internal moisture that conventional mechanical dewatering equipment cannot easily extract, rapidly reducing both the moisture content and total weight of the sludge.
ELODE is an advanced secondary dewatering and sludge-reduction solution designed to overcome the limitations of conventional dewatering equipment within the Glue Zone. By reducing the amount of moisture entering the downstream drying process, it also lowers the required drying load, energy consumption and processing time.
The ELODE Combination System, which integrates ELODE with a downstream drying system, can dry most types of wastewater treatment plant sludge to a final moisture content as low as 10%, equivalent to a solids content of approximately 90%.
Following primary mechanical dewatering, ELODE performs advanced secondary dewatering and sludge reduction within the Glue Zone. The downstream dryer then efficiently removes the remaining moisture.
This integrated process produces a high-solids sludge cake suitable not only for final disposal, but also for fuel production, resource recovery, and recycling.
Conventional thermal dryers generally require approximately 0.95 to 1.20 kWh of energy to evaporate one liter of water.
In contrast, ELODE effectively removes moisture from inside the sludge with a low energy consumption of approximately 0.35 kWh per liter of water removed.
Rather than evaporating moisture using high-temperature heat, ELODE rapidly mobilizes the moisture retained inside the sludge through three electrokinetic mechanisms and discharges it through physical compression.
By reducing the amount of moisture that must be processed by the downstream thermal dryer, ELODE significantly improves the overall energy efficiency of the entire system.
The ELODE Combination System does more than simply reduce energy consumption. By lowering the moisture content, weight, and volume of sludge, it simultaneously reduces drying, transportation, storage, and final disposal costs.
Since less moisture enters the downstream dryer, the required operating time and the consumption of electricity, gas, and steam are also reduced.
As a result, the system lowers operating costs throughout the entire sludge treatment process and maximizes long-term economic efficiency.
Major Cost-Saving Areas
Conventional thermal drying systems may require not only a large-scale dryer, but also auxiliary facilities for heat generation, exhaust treatment, odor control, dust removal, cooling, and safety management. As a result, both the initial capital investment and the required installation area may increase.
ELODE can be installed downstream of existing dewatering equipment, including belt presses, filter presses, screw presses, and centrifuges.
By utilizing the existing facilities, ELODE reduces the need to remove current equipment or construct an entirely new treatment process, thereby minimizing the initial investment burden.
In addition, by reducing the moisture load entering the downstream dryer, ELODE enables the required treatment capacity to be achieved without selecting an unnecessarily oversized thermal dryer.
The ELODE Combination System continuously reduces energy, transportation, and disposal costs, enabling a rapid return on investment.
In particular, facilities that generate large quantities of sludge or face high sludge disposal costs can achieve greater economic benefits.
Although the actual payback period may vary depending on site conditions and sludge characteristics, the system is designed to achieve a target return on investment within 24 months based on a detailed economic analysis.
ELODE removes moisture using significantly less energy than conventional thermal drying methods, thereby reducing the electricity and fuel consumption required by the downstream dryer.
As the weight and volume of the sludge are reduced, the number of transportation trips and the final disposal volume are also decreased.
Through these combined reductions in energy consumption, transportation requirements, and disposal volume, ELODE can establish a low-carbon sludge treatment process that reduces total carbon dioxide emissions by more than 70%.
The three electrokinetic mechanisms of ELODE disrupt the sludge floc structure and weaken the forces retaining free water, bound water, interstitial water, and intracellular water.
This rapidly mobilizes the retained moisture into a readily removable form within approximately 90 seconds.
During this process, even the internal moisture that is difficult to remove using conventional mechanical dewatering alone is effectively discharged. As a result, the moisture content, weight, and volume of the sludge are rapidly reduced.
Through advanced secondary dewatering and downstream drying, the ELODE Combination System can reduce sludge volume by up to 70%, significantly decreasing transportation requirements, storage space, and final disposal volume.
The ELODE Combination System does more than simply reduce sludge volume.
It also provides a safer, cleaner, and more environmentally friendly treatment environment.
BLUEWIN’s 4-NO Principle
By reducing the need to manage dust, odors, and exhaust gases that may be generated during high-temperature thermal drying, the system creates a cleaner and more environmentally responsible sludge treatment process.
Based on a continuous treatment process, ELODE provides fast, stable, and reliable operation. Its automated control system also reduces the operator’s monitoring and management workload.
The system can be flexibly integrated with existing mechanical dewatering equipment and downstream drying systems. Operating conditions can also be adjusted according to the characteristics of the sludge and the target moisture content.
Its robust design and maintenance-friendly structure, developed for long-term operation, provide high operational reliability and an extended equipment service life.
Operational Advantages
The ELODE Combination System produces uniform, high-quality sludge cake with a low moisture content, providing a foundation for converting sludge from waste into a valuable resource.
Depending on the sludge characteristics and local process requirements, the final treated sludge can be utilized for fuel production, composting, biochar production, construction materials, and other resource recovery processes.
In particular, the high solids content reduces the energy demand of downstream resource recovery processes and improves the stability of sludge storage, transportation, and process feeding.
Pressure Alone Cannot Remove the Moisture Retained Inside the Sludge
Conventional mechanical dewatering equipment, including belt presses, filter presses, screw presses, and centrifuges, uses pressure or centrifugal force to remove free water from the exterior of the sludge and form a sludge cake.
These methods are effective for the primary dewatering of large quantities of sludge. However, they have structural limitations when it comes to removing bound water, interstitial water, and intracellular water retained inside the sludge flocs.
In particular, within the moisture content range of approximately 80% to 60%, the sludge enters the Glue Zone, where it develops high viscosity and strong adhesion.
Even when additional pressure is applied, the amount of water discharged does not increase significantly. Instead, the mechanical load and wear on belts, filters, rollers, and drive components may increase.
Key Limitations
They Can Achieve a Low Moisture Content, but Require Significant Energy and Time
Thermal dryers use heat sources such as electricity, gas, and steam to evaporate moisture from inside the sludge, allowing them to achieve a low final moisture content.
However, when sludge with a high moisture content is fed directly into a thermal dryer, a large quantity of water must be evaporated. This significantly increases both drying time and energy consumption.
Highly viscous sludge within the Glue Zone can also adhere to the internal walls and conveying equipment of the dryer. The sludge may agglomerate, resulting in uneven drying and reduced material transfer efficiency.
In addition to the dryer itself, thermal drying systems may require various auxiliary facilities for heat generation, exhaust treatment, odor control, dust management, cooling, and safety. These requirements may increase the initial investment cost and the installation footprint.
Key Limitations
Conventional mechanical dewatering systems have limitations in removing moisture retained inside the sludge,
while thermal dryers consume significant amounts of energy when treating sludge with a high moisture content.
ELODE bridges the gap between these two processes by
performing advanced secondary dewatering and sludge volume reduction w
ithin the Glue Zone, effectively eliminating this inefficient treatment stage.
Category | Conventional Primary Mechanical Dewatering | ELODE | Conventional Downstream Thermal Dryer |
Primary Role | Primary dewatering and sludge cake formation | Advanced secondary dewatering and sludge reduction | Final moisture evaporation and drying |
Operating Principle | Pressure or centrifugal force | Electro-osmosis, electro-infiltration, electrophoresis, and physical compression | Moisture evaporation using thermal energy |
Most Effective Treatment Range | Initial dewatering of high-moisture sludge | The Glue Zone at approximately 80% to 60% moisture content | Final drying to a low moisture content |
Moisture Primarily Removed | External free water | Free water, bound water, interstitial water, and intracellular water | Remaining moisture |
Key Strength | Rapid primary dewatering of large quantities of sludge | Internal moisture mobilization and reduction of moisture content, weight, and volume | Achievement of a low final moisture content |
Key Limitation | Difficulty removing moisture retained inside sludge flocs | None within its designated treatment range | High energy consumption and long drying time |
Process Position | Upstream stage | Downstream of mechanical dewatering and upstream of thermal drying | Downstream of ELODE |
ELODE is not designed to replace mechanical dewatering equipment or completely substitute for a thermal dryer.
Instead, it removes additional internal moisture remaining after conventional mechanical dewatering and reduces the moisture content and weight of the sludge before thermal drying.
In this way, ELODE connects the two processes and allows each system to operate within its most efficient treatment range.
The three electrokinetic mechanisms of ELODE disrupt the sludge floc structure and weaken the binding forces that retain moisture inside the sludge.
This mobilizes free water, bound water, interstitial water, and intracellular water, converting the retained moisture into a more readily removable form within approximately 90 seconds.
Through this process, ELODE effectively discharges internal moisture that is difficult to remove using conventional mechanical dewatering equipment alone.
It also reduces, in advance, the amount of water that the downstream thermal dryer must evaporate.


RFQ
Contact
© 2025 BLUEWIN Co., LTD. All Rights Reserved.


